
 English
 简体中文
 Русский
 Français
 Português
 Español

Freezer warehouses face unique operational challenges that ordinary material handling equipment can hardly address smoothly. The constant low temperature environment, dense high-position storage racks, strict requirements to avoid frozen goods thawing, and limited aisle space all put forward higher standards for the performance of handling equipment, which is why reach forklift has gradually become the core supporting equipment for the optimization of freezer warehouse workflows.
At the goods receiving and storage stage, the compact body design of the reach forklift allows it to travel smoothly in narrow aisles reserved for cold storage, which does not require extra space to widen the aisle, helping the warehouse maximize the effective storage capacity for frozen goods. All core electrical components of the reach forklift designed for low temperature scenarios adopt special sealing and anti-condensation treatment, which can avoid the malfunction caused by frost accumulation in long-term low temperature operation. It can transport the whole pallet of frozen goods to the designated high-rise storage position in one go, no need to transfer goods with multiple devices, greatly shorten the exposure time of frozen goods in the non-low temperature area, and effectively reduce the quality loss of temperature-sensitive goods.
In the daily inventory management and order picking stage, the operation interface of the reach forklift is optimized for operators wearing thick cold-proof gloves, which ensures accurate and flexible operation without misoperation. The optimized battery management system for low temperature environment effectively avoids the sharp attenuation of battery performance in ultra-low temperature scenarios, supports long-time continuous operation in the freezer warehouse, no need to move back and forth to the normal temperature area for battery replacement, which greatly reduces the workflow interruption points. The low-noise operation performance of the equipment will not interfere with other staff working in the same cold storage area, and the operation safety is effectively guaranteed.
At the outbound and inventory checking stage, the reach forklift can flexibly reach every corner of the dense shelf area, quickly complete the whole pallet of goods picking and outbound preparation, and its stable signal connection performance can support smooth data interaction with the warehouse management system, avoid data transmission error caused by low temperature, and improve the accuracy of inventory checking.
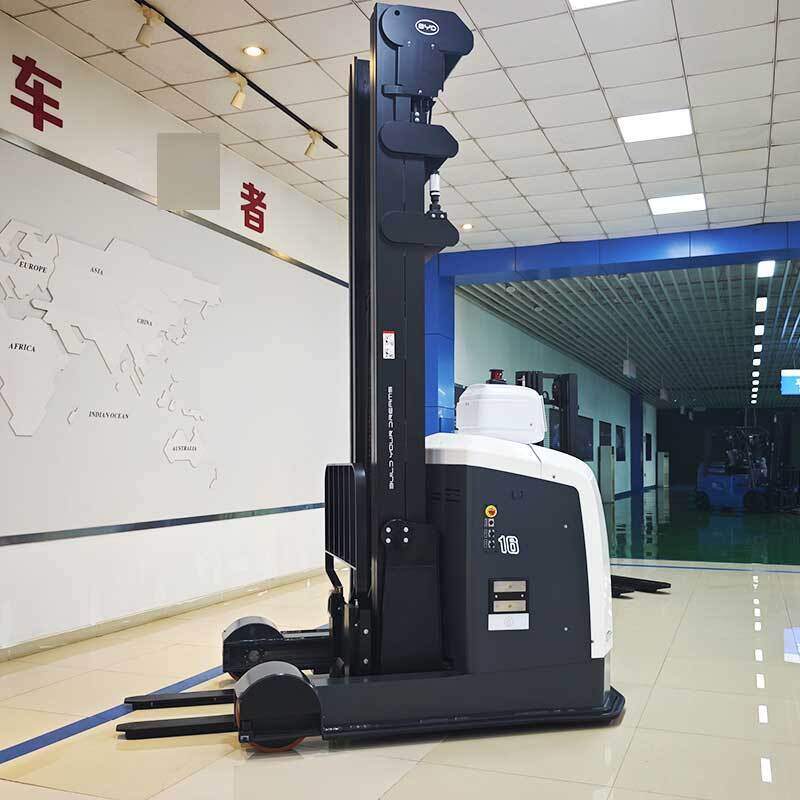
We are Jianshu New Energy, focusing on BYD electric forklifts, and can provide targeted reach forklift matching solutions for different scales of freezer warehouses to help you improve overall operation efficiency. For more information, you can contact us via [email protected].


