English
 简体中文
 Русский
 Français
 Português
 Español

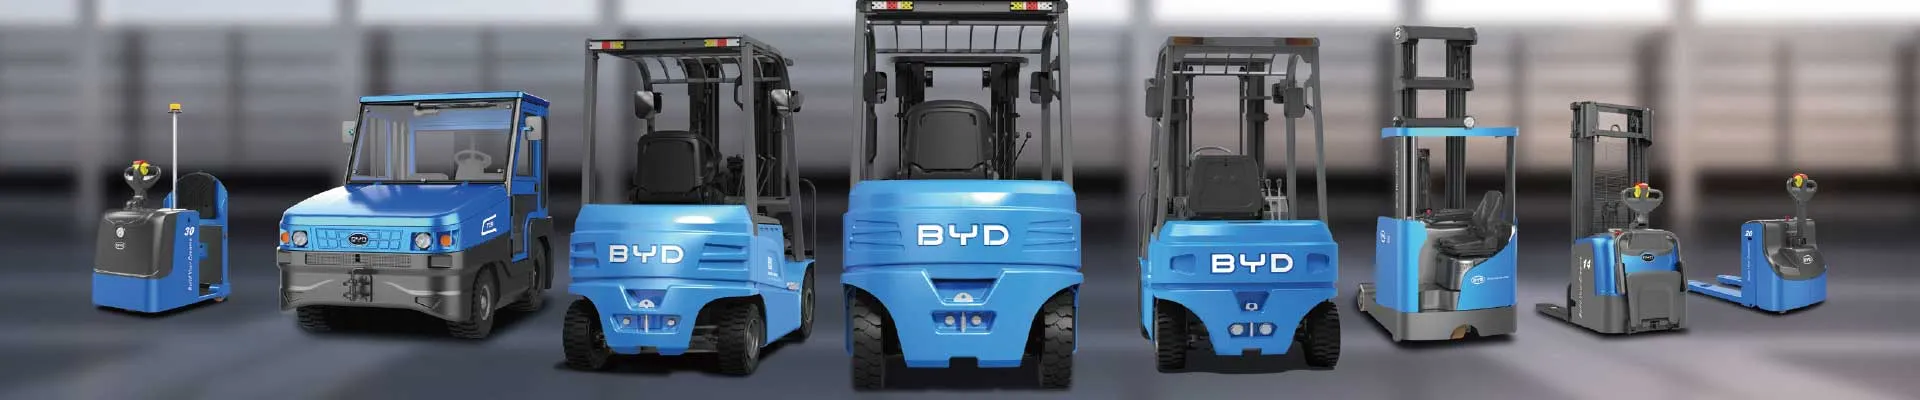
Beverage plants face unique operational challenges across their full production and storage chain, from frequent incoming raw material shipments, high-volume finished product stacking, to fast outbound delivery for distribution networks. Most beverage storage areas are designed with compact narrow aisles and high-position racks to maximize storage capacity for large batches of bottled, canned and boxed beverage products, which puts forward higher requirements for the flexibility and lifting performance of handling equipment.
A reach forklift can well fit the whole workflow of beverage plants starting from the goods receiving stage. After the raw materials or empty packaging pallets are unloaded from the delivery truck, the reach forklift can quickly transfer these heavy loads to the temporary storage area near the unloading platform, with no need for extra wide operating channels, which effectively avoids congestion in the busy receiving zone. Operators can complete the transfer work smoothly even when multiple delivery vehicles unload at the same time in peak hours.
In the high-level storage area of finished products, the core advantage of a reach forklift can be fully exerted. Its telescopic fork design allows operators to accurately place heavy beverage pallets on the racks at heights that common counterbalance forklifts cannot easily reach, without occupying extra aisle space. This feature helps beverage plants increase their total storage capacity considerably in the same limited warehouse footprint, without additional construction investment. As the all-electric reach forklift produces zero exhaust emissions during operation, it will not cause any pollution to food-grade beverage products stored in the enclosed warehouse, which fully meets the food safety management requirements of beverage production enterprises.
When it comes to the production supply and outbound sorting links, the compact body of the reach forklift can flexibly shuttle between the production workshop connection area and the sorting buffer zone, to transport packaging materials to the production line, and move finished pallets to the pre-loading area efficiently. The low-noise operation feature will not interfere with the normal operation of on-site production staff, and the long-lasting battery performance can support continuous operation for multiple shifts that most beverage plants apply.
We are Jian Shu New Energy, focusing on BYD electric forklift products. If you have relevant demands for material handling equipment suitable for beverage plant scenarios, you can send your consultation to [email protected].