
 简体中文
 Русский
 Français
 Português
 Español
 لالعربية

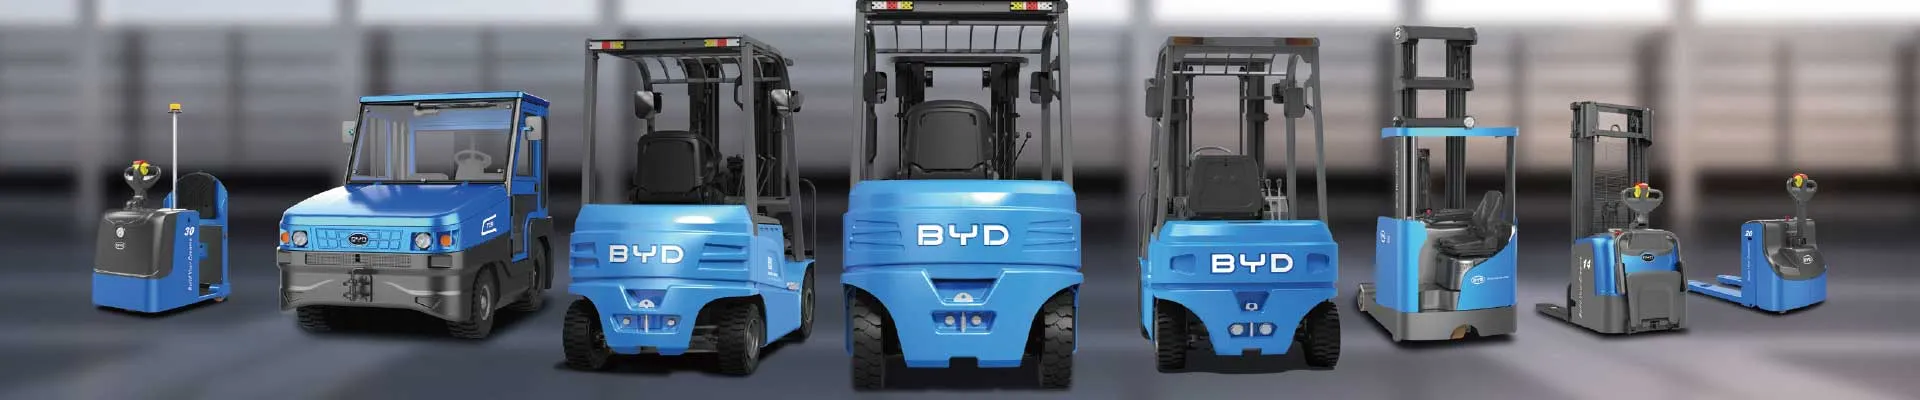
Pharmaceutical warehouses have extremely strict operational standards for material handling, covering hygiene compliance, inventory accuracy, operation stability and personnel safety, which put forward higher requirements for supporting handling equipment. A reach forklift, especially the electric type, can perfectly match the unique operation scenarios of pharmaceutical storage, and brings 6 prominent practical benefits for daily work.
First, it supports high-density narrow-aisle storage to maximize space utilization. Most pharmaceutical warehouses need to store a large number of palletized pharmaceutical products, temperature-sensitive biological preparations and medical supplies. The compact body and extended fork design of the reach forklift allows it to operate smoothly in aisles as narrow as 1.8 meters, which helps warehouse managers to add extra 30% to 40% storage racks under the same floor area, effectively expand available storage space without extra site expansion investment.
Second, zero-emission operation meets strict hygiene and environmental requirements of pharma scenarios. Unlike internal combustion handling equipment, electric reach forklifts produce no exhaust gas, no oil leakage risk and low noise during operation, which will not cause potential pollution to sensitive pharmaceutical products that are sensitive to particulate matter or volatile organic compounds, fully comply with the GMP hygiene standards that all pharmaceutical storage sites need to follow.
Third, precise lifting control ensures the safety of high-value pharmaceutical goods. The optimized hydraulic control system of the reach forklift realizes smooth lifting and lowering operation with minimal jitter, even when handling high-tier storage racks up to 12 meters high, operators can accurately place pallets with expensive biological agents or precision medical devices without collision or goods dropping risk, reduce unnecessary goods loss effectively.
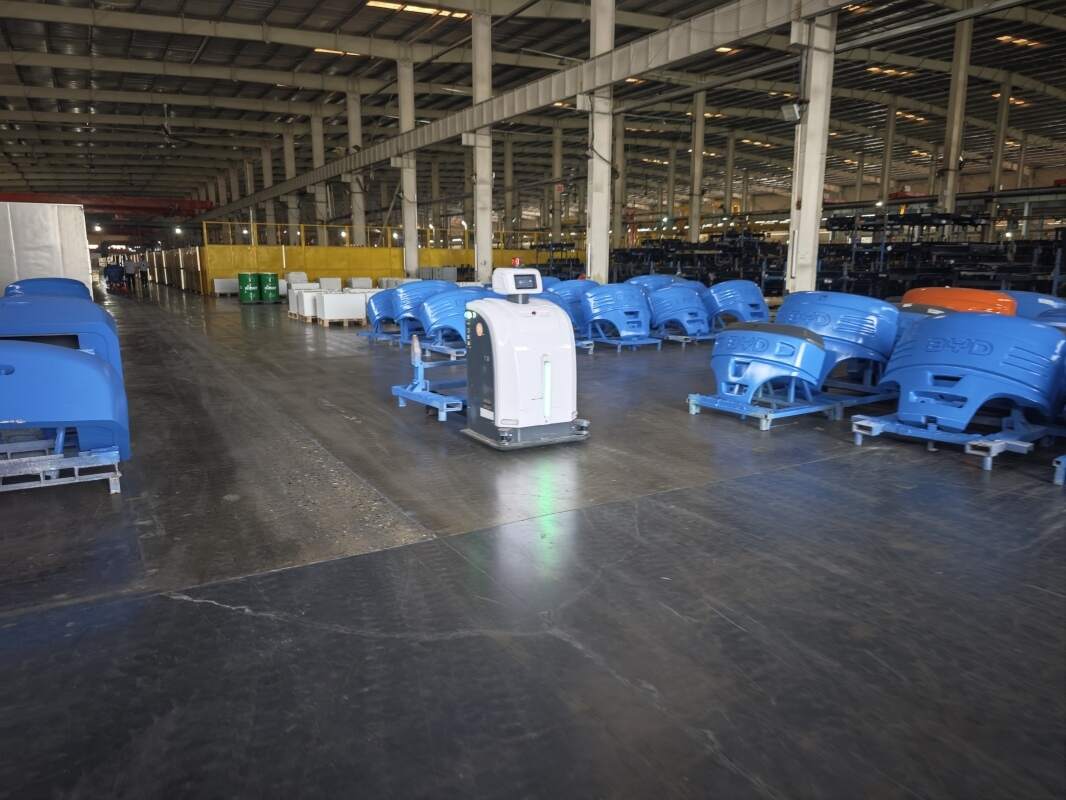
Fourth, it adapts to multi-scenario operation including low-temperature cold storage zones. Many pharmaceutical warehouses are equipped with special cold storage areas for vaccines and biological products that need to be stored at 2-8℃ or even lower temperature. The specially designed electric reach forklift can maintain stable performance in long-term low temperature operation, no extra modification is needed for switching between normal temperature storage zones and cold storage zones, greatly improve the cross-region operation efficiency of the whole warehouse.
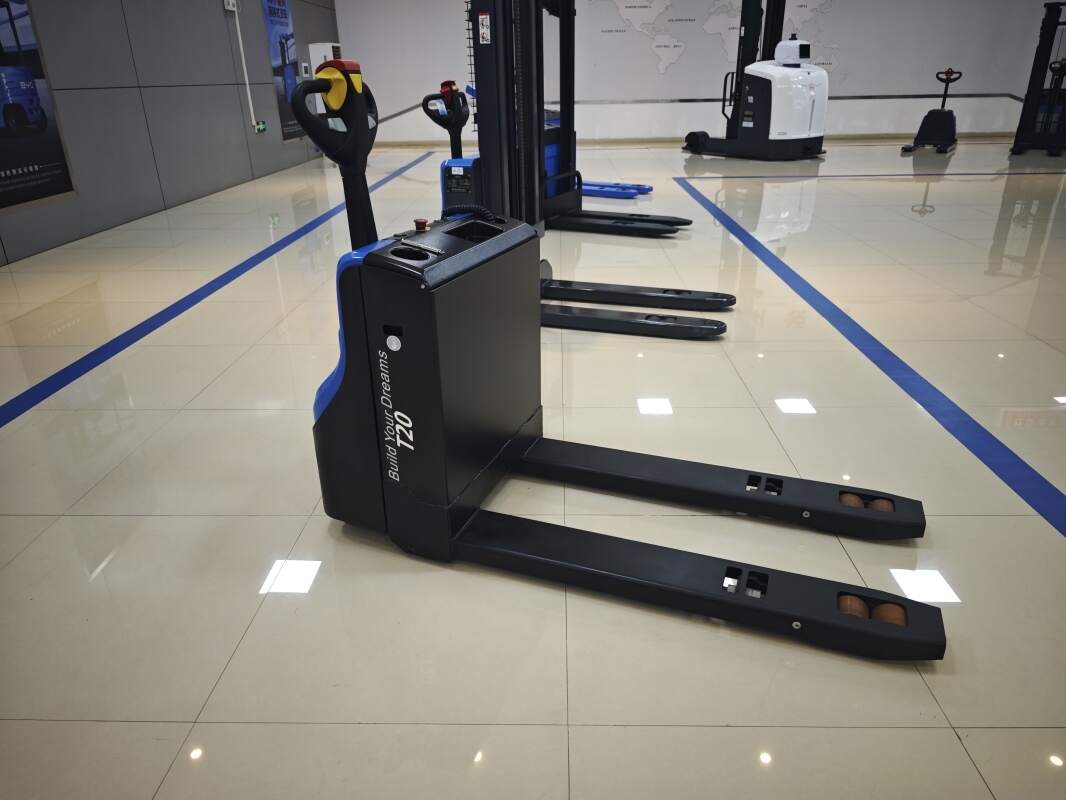
Fifth, it reduces long-term operation and maintenance cost. The electric power system of the reach forklift has no complicated engine structure, the regular maintenance work only covers battery inspection, brake and fork parts check. Compared with traditional fuel handling equipment, it can cut down more than 50% of daily maintenance cost in the whole service life, and bring more stable cost control effect for warehouse operation.
Sixth, it helps to improve overall operation safety compliance. The reach forklift is equipped with multiple built-in safety configurations including overload protection, anti-slip function for high tier operation, automatic speed limit in narrow aisles, which effectively reduce the operation safety risks in high-density pharma storage sites, and help the site pass the regular safety inspection smoothly.
As a professional new energy material handling solution provider, Jianshu New Energy focuses on BYD electric forklifts, if you have any demand for handling equipment suitable for pharmaceutical warehouses, you can send an email to [email protected] for further consultation.


