English
 简体中文
 Русский
 Français
 Português
 Español

Food and beverage facilities have unique operational requirements that set them apart from regular general warehouses, especially when it comes to material handling equipment that operates across raw material storage, semi-finished product staging and finished goods distribution zones. A reach forklift, as the core equipment for high-rack storage and inventory sorting, needs to match the special operation scenarios of the industry to support stable, compliant daily operation.
First of all, full compliance with food safety and hygiene standards is the top priority for reach forklifts used in food and beverage facilities. The equipment surface needs to adopt smooth, non-porous coating that is easy to wipe and disinfect, without hidden gaps that may accumulate food residues, dust or mold. All parts that may come into indirect contact with packaging materials should not shed debris, and the operation system will not produce any oil leakage or excess particulate emissions that may pollute stored goods. The chassis design also reserves enough cleaning space for facility staff to regularly wash the ground below the vehicle, avoiding hidden hygiene risks.
Many food and beverage facilities are equipped with constant temperature and cold storage areas to keep perishable ingredients and finished products fresh, so the reach forklift needs to support stable operation in low temperature environments for a long time. The power system, operation control module and display screen can maintain normal working performance even in cold scenarios, without frequent shutdown or sensitivity reduction, so that the efficiency of inbound and outbound operation will not be affected. Unlike fuel-powered equipment, the pure electric design will not produce exhaust gas that may affect the flavor and quality of stored food, which is more suitable for enclosed storage spaces.
Flexible operation and low noise performance are also essential attributes for applicable reach forklifts. Most food and beverage facilities arrange production and storage operation in overlapping zones, and the low noise operation of the electric reach forklift will not interfere with normal production staff work, nor will it cause vibration that affects the placement of fragile packaged goods. The narrow aisle adaptation design can make full use of the limited storage space in the facility, increase the density of high-rise racks, and help enterprises improve the utilization rate of warehouse area. The reasonable power management system can support long hours of continuous operation to cope with the peak period of goods delivery and inventory sorting.
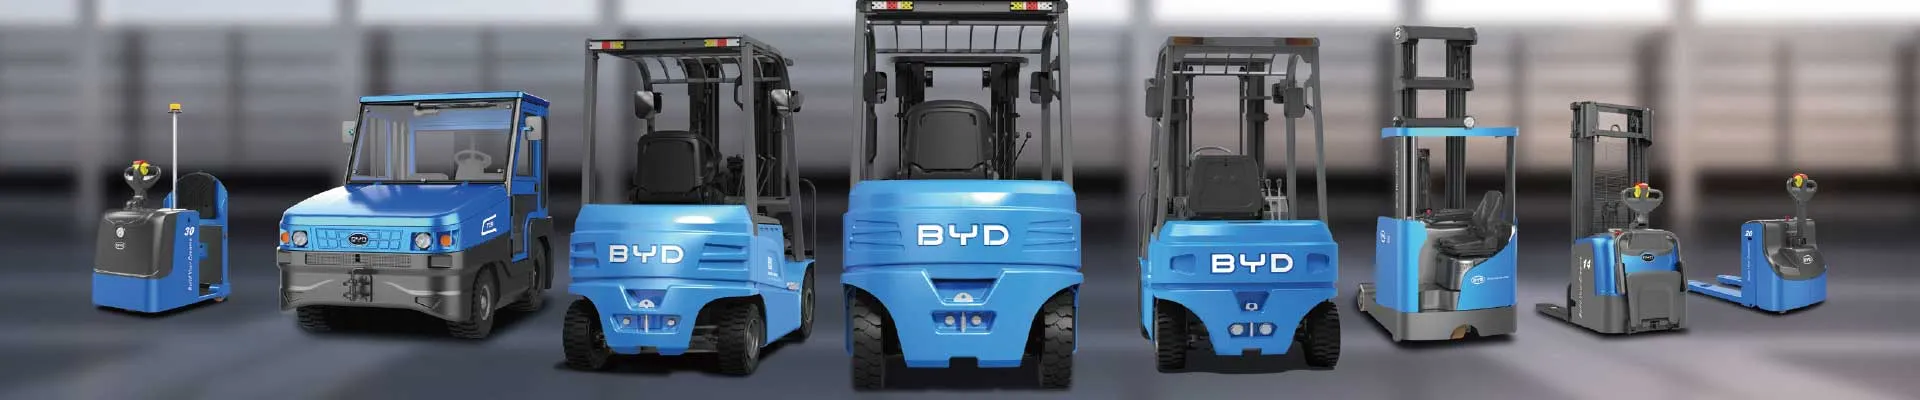
As Jianxin New Energy, we focus on supplying high quality BYD electric forklifts that fully match the above demands for food and beverage industry scenarios. If you have related demand for material handling equipment, you can contact us via [email protected] for more detailed solution support.