简体中文
 Русский
 Français
 Português
 Español
 لالعربية

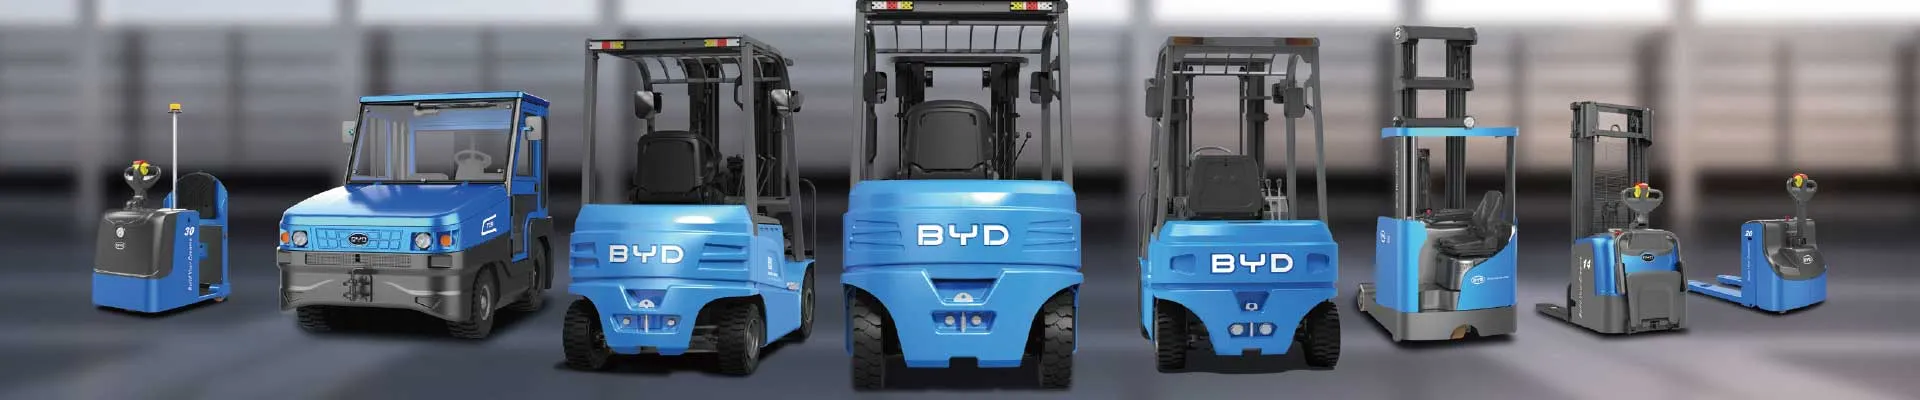
Beverage production plants have unique operational characteristics different from ordinary manufacturing scenarios. First, most finished beverage products are packaged in bottles, cans or cartons, which are relatively heavy after being stacked on pallets, and the whole site needs to meet food-grade hygiene management standards. Second, most beverage plants have high requirements for storage capacity, and many warehouses adopt high-shelf design to maximize storage capacity, while the reserved working channels between shelves are relatively narrow. Third, the order delivery volume of the beverage industry fluctuates greatly with seasons and promotional nodes, requiring the logistics link to maintain stable and efficient operation even in peak periods.
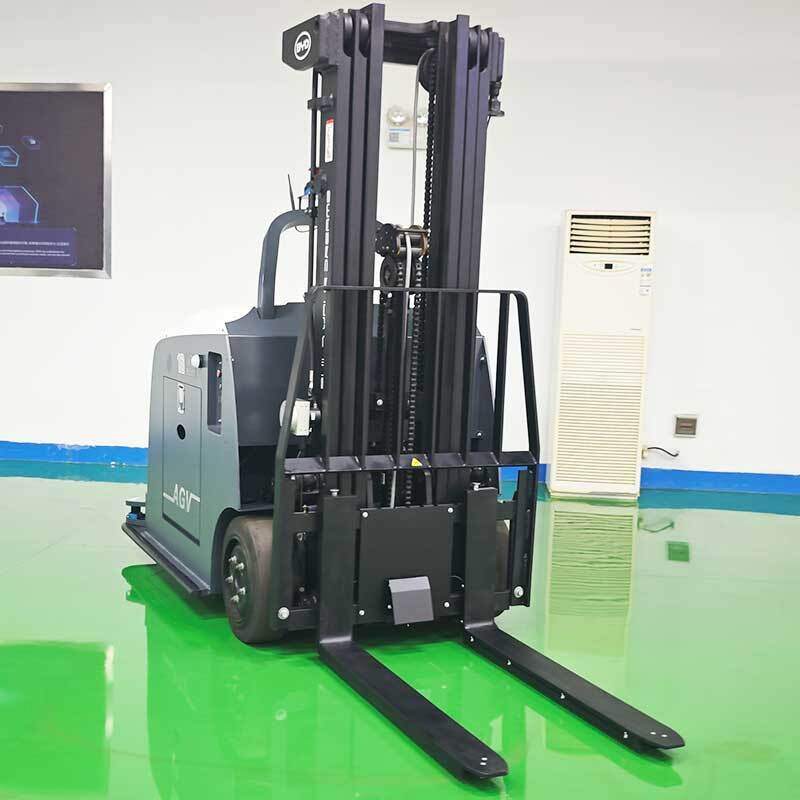
Under such operational background, the reach forklift has become a core handling equipment widely used in the storage area of beverage plants. First of all, it can well adapt to the narrow channel and high shelf operation scenario. The body design of the reach forklift does not need too much turning space, which can operate smoothly in the narrow channel reserved for high shelves, and its stable lifting performance can meet the storage and access requirements of pallets at different heights of high shelves. This feature can help beverage plants make full use of the vertical space of the warehouse, expand the total number of storage positions without expanding the warehouse area, and effectively reduce the additional cost of storage capacity expansion.
Secondly, the electric reach forklift fully meets the hygiene and environmental protection requirements of food processing plants. It does not produce exhaust gas in the working process, and there will be no oil stain or peculiar smell residue around the operation area, which will not cause potential pollution to the stored beverage products, and will not affect the sanitation standard of the finished product storage area. At the same time, the low-noise operation feature also improves the working environment of on-site operators, and avoids the noise interference caused by traditional internal combustion handling equipment to the surrounding production and office areas.
In addition, the reach forklift with precise operation performance can effectively reduce the cargo damage rate in the handling process. The packaged beverage products have certain fragility, and slight collision may cause damage to the outer package or even leakage of the inner product. The reach forklift can complete the alignment and access of the pallet stably during the handling process, effectively reduce the collision between the goods and the shelf, and reduce the unnecessary loss of finished products. In the peak season of product delivery, it can also help the logistics team quickly complete the outbound and replenishment operations, and maintain the stable operation of the whole supply chain.
As Jianshu New Energy, we focus on BYD electric forklift, and can provide targeted handling equipment selection schemes for beverage plants of different scales. If you have relevant consultation demands, you can send an email to [email protected] for further communication.