简体中文
 Русский
 Français
 Português
 Español
 لالعربية

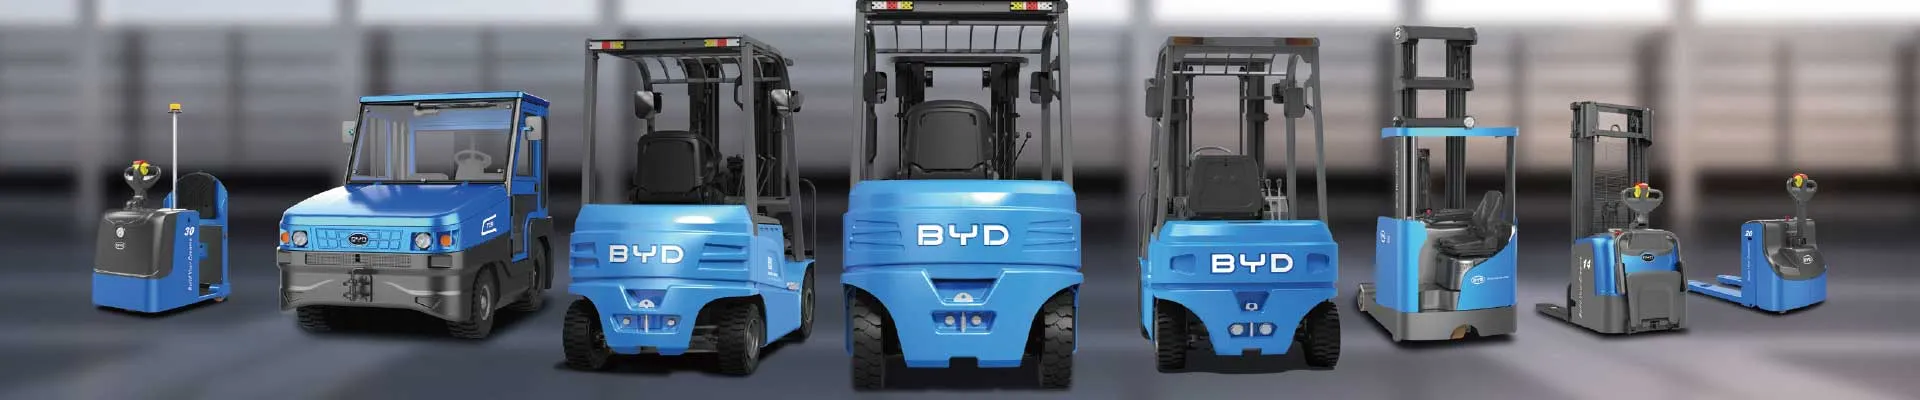
Beverage production facilities face unique material handling demands across their entire operation workflow, from raw material storage in the upstream section, finished product transit between production lines, to high-density pallet stacking in the finished goods warehouse. Most beverage manufacturing scenarios require frequent, high-load handling tasks that run through whole shifts, while the operational environment puts forward strict requirements for equipment safety, hygiene and environmental performance.
The electric counterbalance forklift is a highly suitable solution targeting these practical demands. With its mature counterweight design, the equipment can deliver stable load-bearing performance to support safe stacking and picking of palletized beverage goods on different height levels, which fits the common high-position rack layout in most modern beverage plants well. As a full-electric driven equipment, it produces zero exhaust emission during operation, with no risk of oil leakage or residual waste gas that may cause potential pollution to food and beverage products, fully complying with the food production hygiene management specifications.
For the frequent wet ground situation in beverage production workshops caused by condensed water or raw material spillage, the electric counterbalance forklift is equipped with optimized anti-slip system to lower slipping risk during operation. Its low-noise operating feature will not cause extra interference to the normal production scheduling and on-site communication, and the reliable battery performance can support continuous operation for a full shift to meet the high-frequency handling demand without frequent energy supplement.
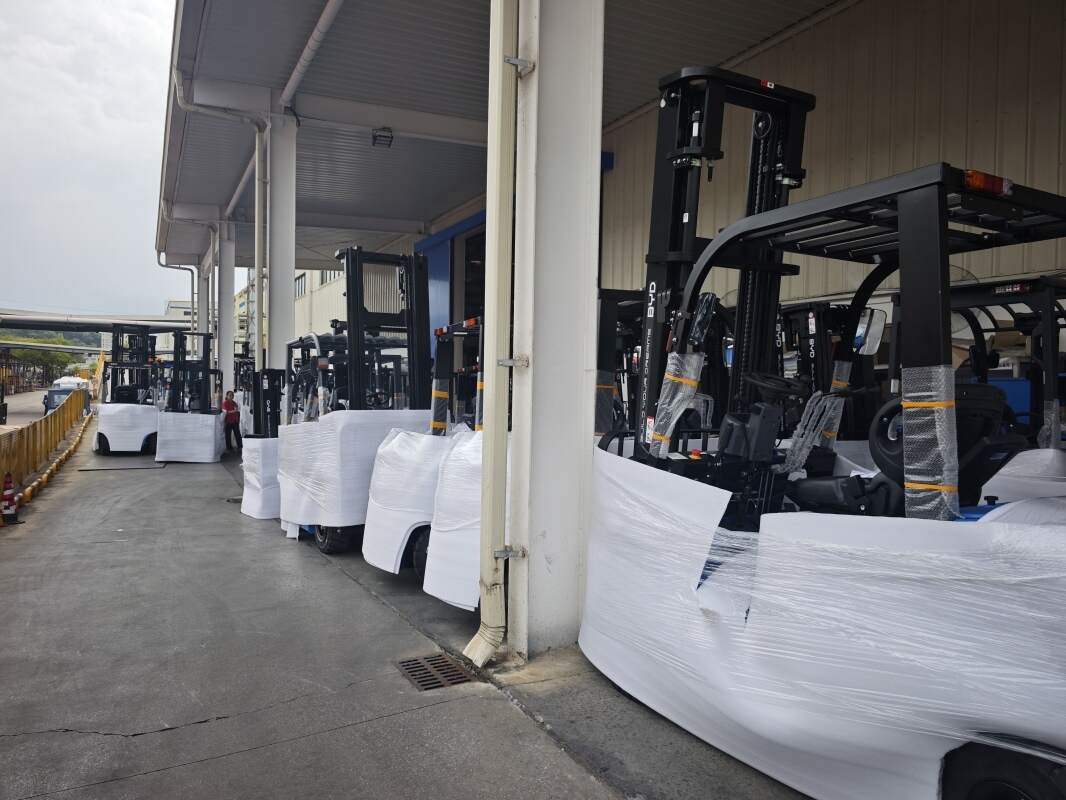
We are Jianshu New Energy, focusing on BYD electric forklift products. We can provide targeted, practical customized material handling solutions for beverage plants of different scales. If you have relevant consultation demands, please send email to [email protected] to connect with our professional service team.