简体中文
 Русский
 Français
 Português
 Español
 لالعربية

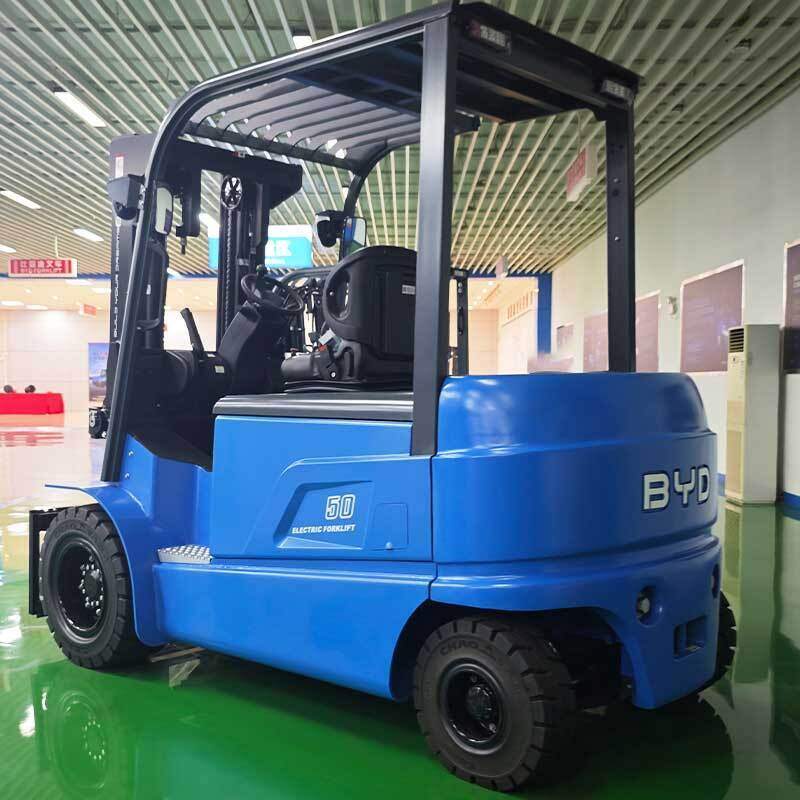
Pharmaceutical warehouses have unique and standardized operation requirements that differ from ordinary industrial storage scenarios. First of all, the storage environment needs to maintain a clean, emission-free state to avoid contamination of pharmaceutical products including finished drugs, raw materials, and biological reagents. Meanwhile, the operation process requires high handling stability and precision, to prevent damage to temperature-sensitive, fragile or high-value pharmaceutical batches during transportation and stacking.
A qualified counterbalance forklift can perfectly adapt to these demands with targeted design features. First of all, the electric-powered counterbalance forklift produces no exhaust gas or harmful emissions during the whole operation process, which will not cause any potential pollution to the stored pharmaceutical products, and fully meets the clean environmental control standards of pharmaceutical sterile storage areas. Compared with internal combustion handling equipment, it also eliminates the need for additional waste gas treatment facilities in the warehouse, reducing extra operation management costs.
Second, the counterweight design of this type of forklift provides reliable operation stability. When handling pallets with different load weights, the equipment can maintain a stable body state, avoid shaking or tilting in the process of transporting high-value pharmaceutical cargo, and reduce the risk of cargo damage. The accurate control performance also allows operators to complete high-position stacking operations on high-level storage racks stably and accurately, making full use of the limited storage space of the pharmaceutical warehouse, and facilitating the classified storage of different batches of pharmaceutical products.
Third, the electric counterbalance forklift runs with low noise and low vibration, which will not interfere with the normal operation of precision temperature and humidity monitoring instruments widely arranged in the pharmaceutical warehouse, and will not cause extra vibration impact on special pharmaceutical products that have strict shock resistance requirements. Its low maintenance demand also reduces the downtime caused by equipment inspection and maintenance, and can support multi-shift continuous operation to match the normal operation rhythm of pharmaceutical warehouses.
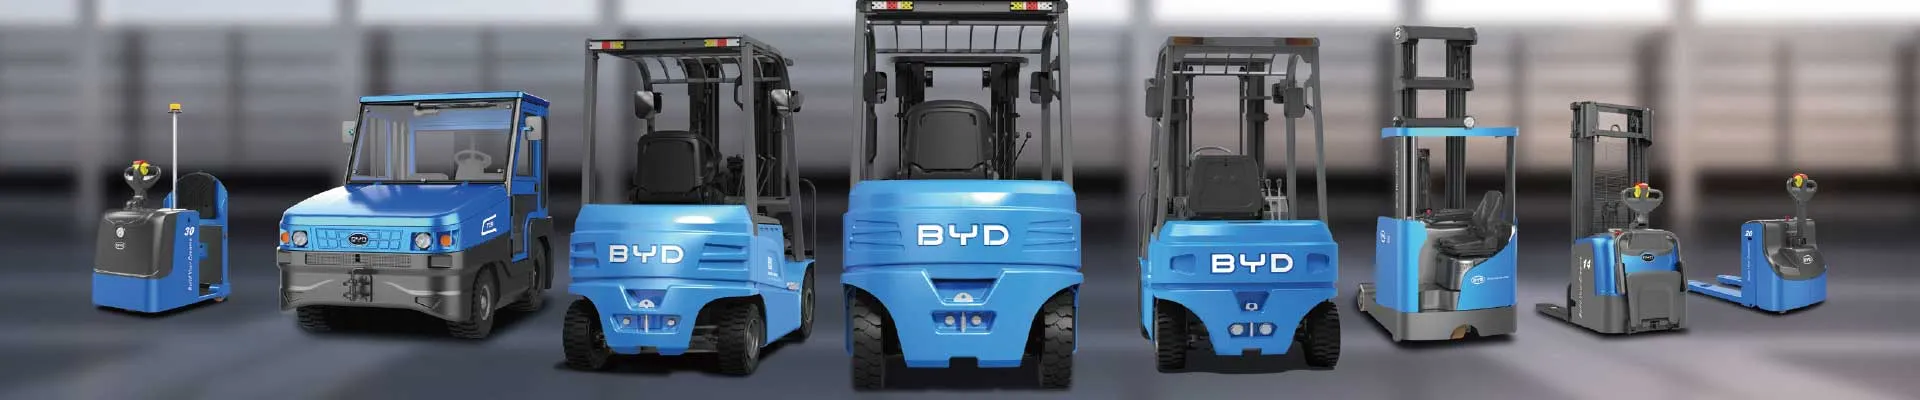
We are Jianxin New Energy, focusing on BYD electric forklift solutions for different industrial scenarios. If you have relevant demand for handling equipment that adapts to pharmaceutical warehouse operation, you can contact us via [email protected] for more detailed information.