
 简体中文
 Русский
 Français
 Português
 Español
 لالعربية

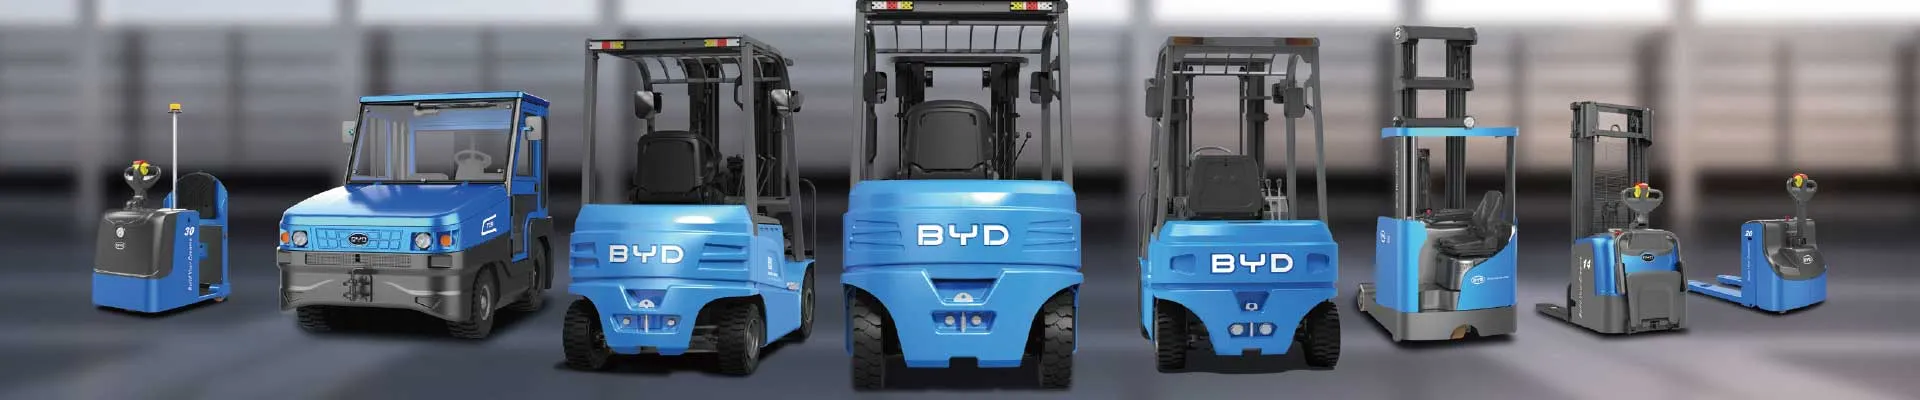
Beverage production plants have unique material handling demands, ranging from moving raw ingredient pallets, finished bottled and canned product stacks to loading and unloading delivery fleets, which requires handling equipment that fits strict food safety, efficiency and cost control requirements. The 12 practical benefits of electric forklifts for such scenarios are listed below:
First, zero local exhaust emissions. No exhaust waste will be generated during operation, avoiding any risk of contaminating unpackaged beverage raw materials or semi-finished products in the production zone. Second, extremely low operation noise. The noise level of electric forklifts during operation is far lower than that of traditional internal combustion forklifts, which will not interfere with normal work of production line staff and reduce occupational noise exposure risks. Third, lower long-term energy cost. Electric power as energy source has more stable unit cost compared with conventional fuel, and the overall energy expenditure per hour of operation can be effectively controlled. Fourth, minimal maintenance demands. The power system structure of electric forklifts is simpler, there is no need for regular replacement of engine oil, filter elements and other consumables required for internal combustion equipment, cutting down maintenance time and related cost. Fifth, stable and consistent power output. The electric drive system can maintain steady power performance even in frequent start-stop, short-distance moving scenarios which are common in beverage plants. Sixth, no fuel leakage risk. Without traditional fuel storage and supply structure, electric forklifts avoid the hidden danger of fuel leakage that may pollute beverage products and ground cleaning systems. Seventh, cross-scenario applicability. Electric forklifts can be used both in closed indoor production workshops and outdoor loading and unloading yards, no extra emission control modification is needed. Eighth, multiple fast charging options. Users can arrange supplementary charging during off-peak production hours, no need to reserve long time for dedicated refueling process. Ninth, enhanced operator comfort. The vibration level of electric driving is much lower, which reduces operator fatigue during long shifts of handling heavy beverage pallets. Tenth, food safety regulatory compliance. The operation features of electric forklifts fully meet the strict food contact environment management rules for food and beverage production sites. Eleventh, longer expected service life. Properly maintained electric forklifts can deliver stable performance for long operation cycles, reducing the frequency of equipment update investment. Twelfth, higher residual value. Well-maintained new energy electric forklifts retain good residual value in the secondary industrial equipment market at the end of usage period.
As a professional new energy material handling solution provider, Jian Shu New Energy focuses on high-performance BYD electric forklifts, if you have relevant demand for equipment matching, please contact us via [email protected].


