English
 Русский
 Français
 Português
 Español
 لالعربية

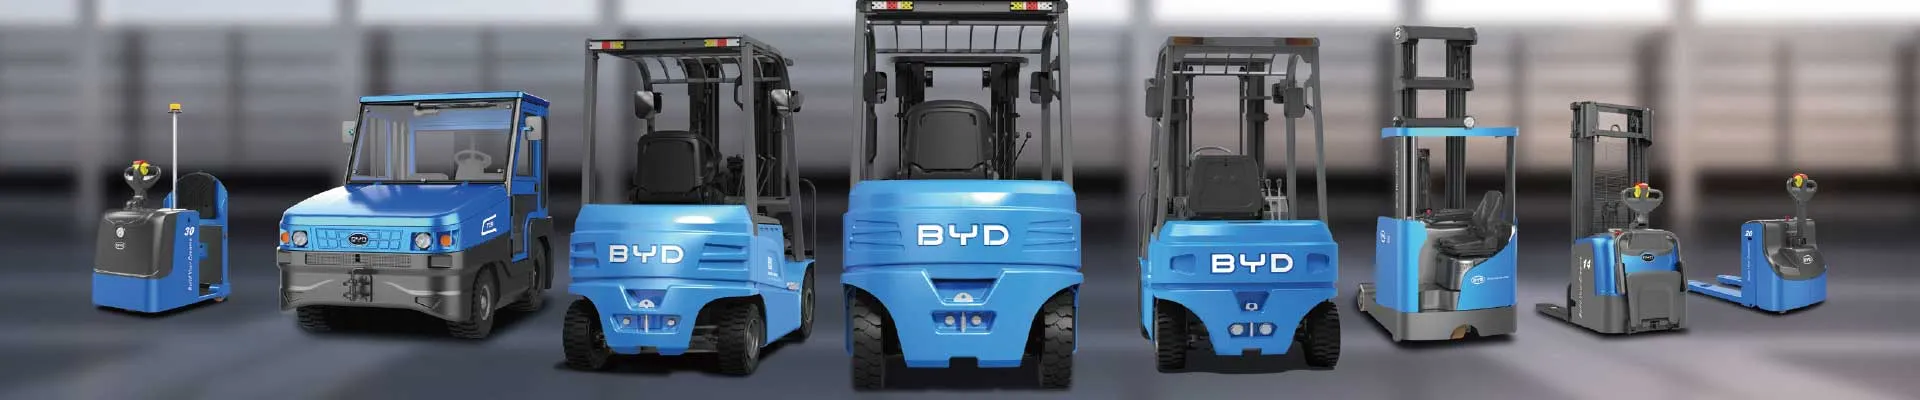
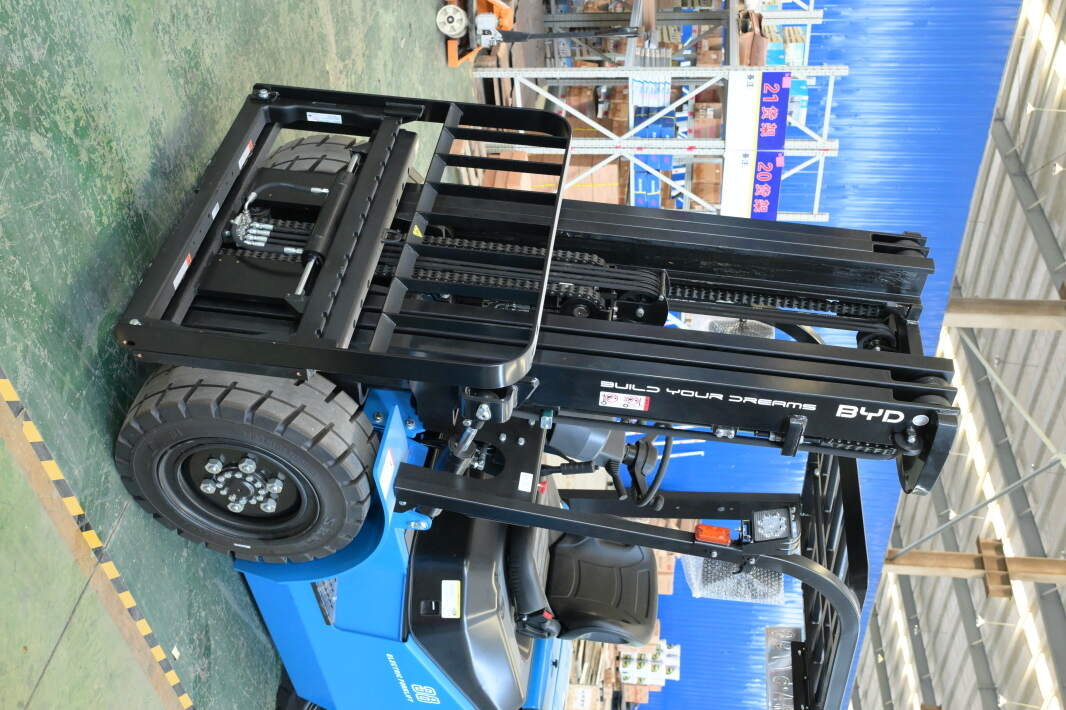
Pharmaceutical warehouses have strict management rules covering GMP compliance, environmental cleanliness, operation safety and goods damage control, which puts forward higher requirements for internal material handling equipment. As one of the most widely used core handling tools, the counterbalance forklift needs to meet multiple special demands unique to the pharmaceutical industry rather than only meeting ordinary storage operation needs.
First of all, pharmaceutical warehouses have zero tolerance for pollutant emissions. Traditional internal combustion counterbalance forklifts will produce exhaust gas, and there is a risk of lubricating oil leakage during long-term operation, which may cause hidden pollution to raw pharmaceutical materials, semi-finished products and finished drugs. The electric counterbalance forklift with full power drive has no exhaust emission, no oil leakage risk after strict sealing treatment, which can fully adapt to the clean environment requirements of pharmaceutical storage areas, and will not introduce extra pollution sources that affect drug quality.
Secondly, the operation stability of counterbalance forklifts is very important for pharmaceutical warehouse scenarios. Most of the stored pharmaceutical products are high-value goods, and many warehouses adopt high-level shelf storage design. The electric counterbalance forklift has sensitive and smooth control performance, stable braking system, which can effectively avoid cargo collision, drop and damage in the process of stacking and handling, reduce unnecessary operation loss, and ensure the integrity of pharmaceutical products in the whole handling link.
Third, counterbalance forklifts for pharmaceutical scenarios need to match special safety configuration according to the actual situation. For storage areas with special requirements such as anti-static and explosion-proof, the electric counterbalance forklift can be adjusted with corresponding electrical system protection, anti-static body coating and other configurations, which fully meets the safety operation specifications of the pharmaceutical industry, and avoids potential safety hazards in high-standard storage areas.
In daily operation and management, warehouse managers also need to make regular plans for forklift body cleaning, battery status inspection, and staff operation training, to ensure that the equipment always meets the access standards of pharmaceutical storage areas, and maximize the operation efficiency of handling links. We are Sharp Tree New Energy, focusing on BYD electric forklift, and can provide targeted counterbalance forklift matching solutions for different pharmaceutical warehouse scenarios. If you have related demands, please send emails to [email protected] for consultation.