
 English
 简体中文
 Русский
 Français
 Português
 Español

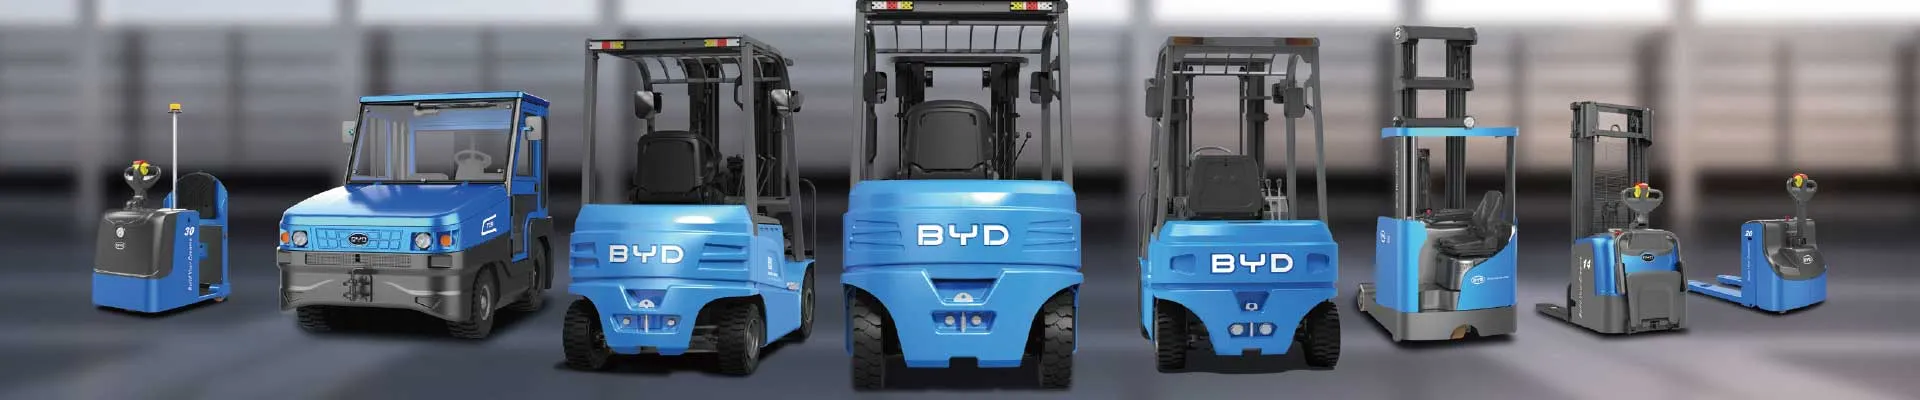
Against the general trend of low-carbon transformation of material handling equipment, lithium-ion powered forklifts have gradually replaced traditional lead-acid and internal combustion forklifts as the preferred configuration for most warehouse, manufacturing and port operation scenarios. Many procurement teams often face a confusing choice when formulating equipment renewal plans: choosing a cost-competitive new lithium forklift brand that has recently entered the track, or choosing a mature global brand that has been operating in the material handling field for decades.
From the perspective of procurement risk assessment, new-brand lithium forklift products usually have obvious advantages in initial input cost, and many new entrants launch flexible cooperation terms to attract target customers. But most new brands have a short industrial chain operation cycle, and the long-term reliability data of core components such as lithium battery packs and motor controllers under high-intensity working conditions is not fully verified. Purchasers need to make additional investigation on the continuous operation qualification of the supplier, to avoid the situation of unable to get follow-up component supply if the brand stops operation in a short period. For established global brands, the main procurement risk comes from the relatively high initial procurement cost, and the response cycle for personalized customized demand for non-standard working conditions is longer than that of local new brands, which may affect the overall equipment deployment schedule of the project.
From the dimension of post-purchase support, most new lithium forklift brands will build a localized small service team, which can reach the site quickly after receiving the fault feedback. However, due to the lack of long-term fault case accumulation, the service team may not have enough targeted solutions for abnormal faults under special working conditions such as low temperature cold storage and high dust factories. The after-sales system of established global brands has undergone decades of iterative optimization, with a complete global parts reserve system and standardized fault handling process, which can ensure the consistency of service quality in most conventional scenarios. For some remote operation areas that are not included in the core business layout of global brands, the service response efficiency may be lower than that of local new brands.
Before finalizing the procurement plan, the procurement team can combine the actual operation intensity of the site, the budget reserve and the self-owned operation and maintenance capacity to conduct multi-dimensional inspection of suppliers, so as to select the most suitable equipment solution for their own operation scenarios.


