
 English
 简体中文
 Русский
 Français
 Português
 Español

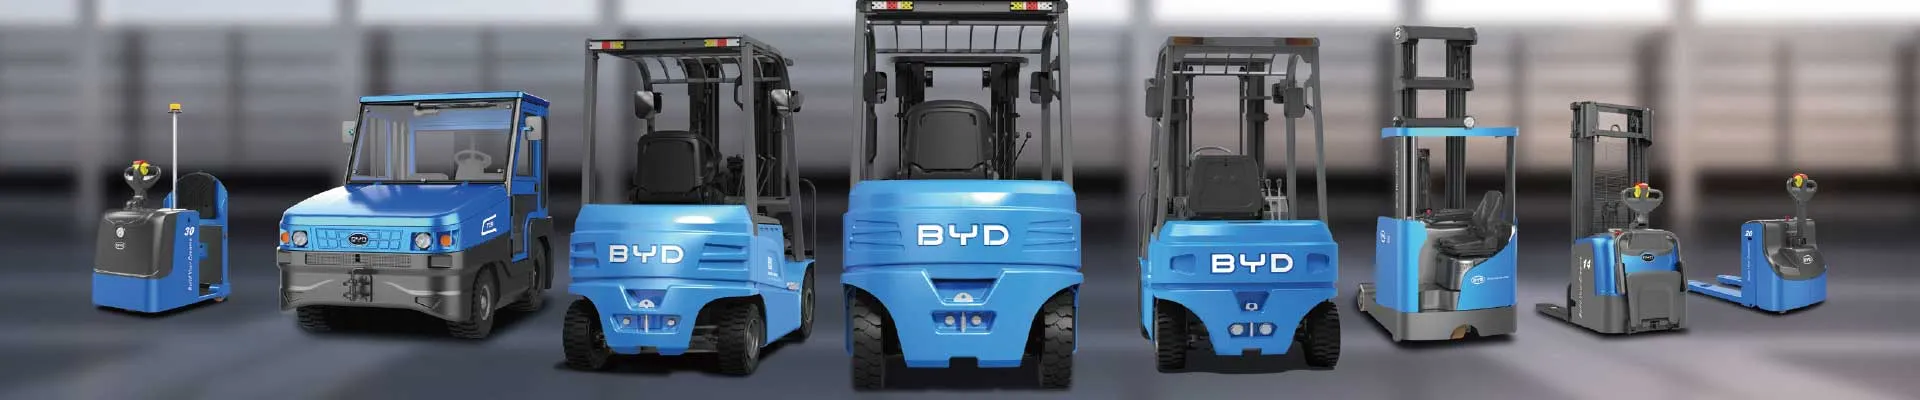
For most large domestic manufacturing plants, in-plant material handling is one of the core links that directly affect production line operation efficiency. For a long time, many manufacturing sites faced common pain points in traditional material handling equipment: exhaust emission does not meet the closed workshop environmental protection standards, frequent battery replacement of old equipment occupies extra production area, and insufficient continuous operation capacity often leads to waiting for handling at peak production periods.
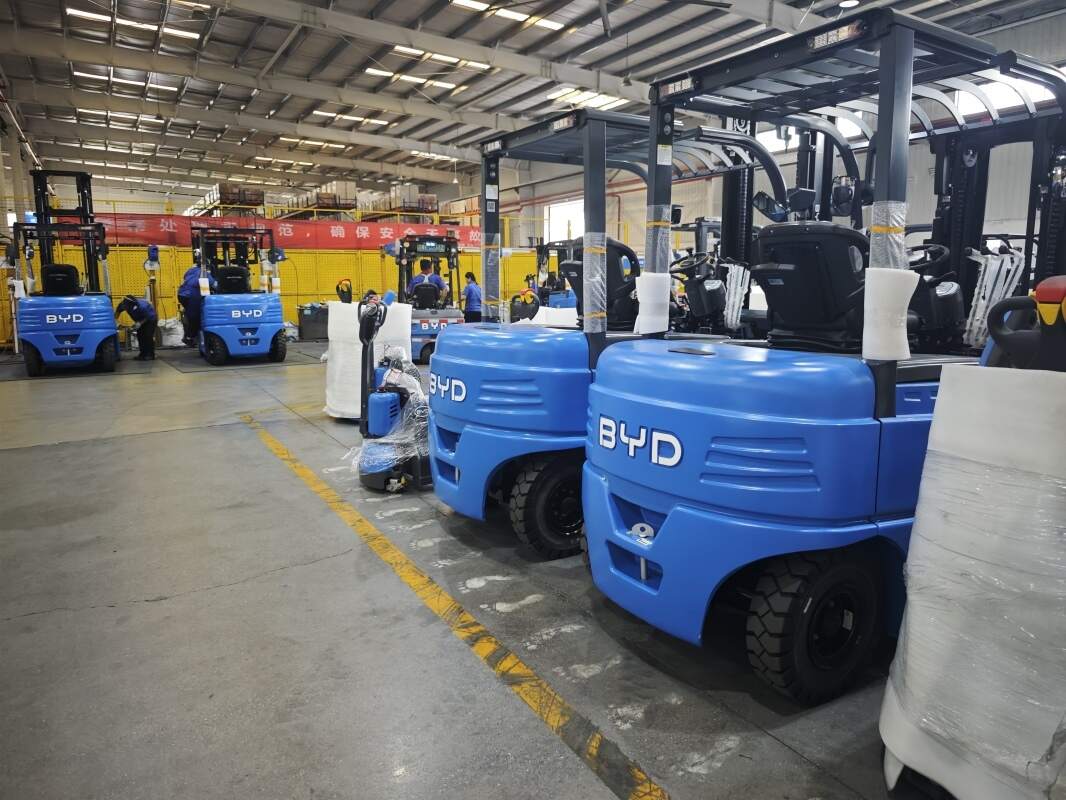
The case shared in this paper comes from a large-scale heavy equipment parts manufacturing plant, which implements three-shift 24-hour production mode. The plant covers an area of more than 120,000 square meters, with more than 120 fixed material moving routes connecting raw material warehouse, stamping workshop, assembly workshop, finished product warehouse and delivery port, with average daily handling tasks exceeding 1,600 times. Before deploying the new fleet, the old handling equipment could not meet the growing operation demand, and the annual comprehensive operation and maintenance cost of the fleet remained at a high level.
Before the formal deployment of BYD lithium-ion forklift fleet, the professional service team completed 30 consecutive days of on-site working condition survey, counted the load demand, operation frequency, channel width, ambient temperature and operation intensity of each handling route, and matched different tonnage of lithium-ion forklifts for different scenarios. The team also designed the distributed fast charging points, which are arranged in the corner of non-core moving lines, and will not occupy the production and passage space of the plant.
After the formal delivery and operation of the fleet, the actual operation data shows that the lithium-ion forklift can complete 4 hours of continuous operation after 1 hour of fast charging, and the power supplement can be completed in the gap between shifts, no special personnel is needed to be arranged for battery replacement and maintenance on duty. The zero-emission, low-noise feature completely eliminates exhaust pollution in the closed workshop, and the working environment of front-line workers is significantly improved. The supporting intelligent fleet management system can track the operation status, remaining power and maintenance reminder of each device in real time, and the scheduling personnel can dynamically adjust the vehicle allocation according to the peak period of handling tasks.
After 6 months of stable operation, the plant’s comprehensive energy consumption cost of the material handling fleet decreased by nearly 40%, the average delivery efficiency of in-plant materials increased by 22%, and no long-term production line shutdown accident caused by handling equipment failure occurred during the operation period. This case verifies that the reasonable deployment of BYD lithium-ion forklift fleet can bring stable and considerable value of cost reduction and efficiency improvement for manufacturing enterprises.


